 English
 русский
 عربى

Features of a Stainless Steel Wire Drawing Machine That Decide the Finish
A matte surface, an oval cross-section or a coil that work-hardens past its limit cannot be corrected at the take-up. These are the machine features that decide whether stainless wire leaves the die box clean, round and on size.
The moment a drawing line switches from low-carbon steel to 304 or 316 stainless, the symptoms arrive quietly. The wire comes off the capstan slightly matte. Die wear that was previously predictable accelerates inside a single shift. Diameter drifts a few hundredths of a millimetre, and a coil is scrapped for a reason that never registers as a machine fault.
The features of a stainless steel wire drawing machine that control this are unglamorous: submerged die cooling, filtered lubricant, capstan surfaces that grip without scoring, and tension control steady enough to hold a hundredth of a millimetre. Rated line speed is the last variable worth optimising and usually the first one buyers ask about.
Why Stainless Behaves Differently Inside the Die Box
Stainless steel work-hardens as it is reduced. Its resistance to deformation climbs with every pass, so a motor that pulls 1.0 mm low-carbon wire without strain will labour on stainless of the same gauge. The usual answer is a lighter reduction schedule: roughly 10 to 18 percent per pass for stainless, against 20 to 25 percent for low-carbon wire.
Lighter passes mean more dies, a longer drawing sequence, more heat distributed along the machine, and far less tolerance for anything that disturbs alignment or lubrication. A handful of machine features carry most of that load.
| Requirement | Machine feature that answers it | What to verify |
|---|---|---|
| Heat at the die | Wet drawing with submerged dies in a water tank | Tank volume, flow per die, temperature band |
| Surface finish | Polished carbide dies, small reduction per pass | Pass schedule, die count, approach angle |
| Lubricant condition | Recirculating emulsion with filtration and cooling | Filter rating, sump capacity, heat exchange |
| Tension stability | Dancer or accumulator control with fast torque response | Tension accuracy at speed changes |
| Spool quality | Accurate traverse and rigid spool mounting | Traverse repeatability, spool runout |
| Break recovery | Wire break detection with fast braking | Stopping time, length of scrapped wire |
Wet Drawing Geometry, Die Cooling and Lubricant Flow
Below roughly 1.2 mm, stainless wire is almost always drawn wet. The dies sit submerged in an emulsion that carries heat out of the reduction zone, lubricates the contact area and flushes metal fines clear of the die. Dry drawing can be made to work on heavier stainless, but the difference usually shows up in surface quality and die life rather than in the speed figure.
Die temperature is the strongest single influence on finish and tooling life. A water-cooled mould box holds the die holder at a stable temperature and keeps the seating surfaces from expanding unevenly, which is what produces ovality late in a long run. Ask how cooling reaches each die position, not just the tank.
Lubricant Cleanliness and Temperature
Once a line runs wet, the emulsion becomes a process fluid with a specification. Metal fines that the filtration misses are dragged back through the die and score the wire; emulsion running warm loses film strength exactly where the pressure is highest. Filtration rating, sump volume, pump flow and temperature control are machine features to be quoted, not maintenance chores to be discovered later.
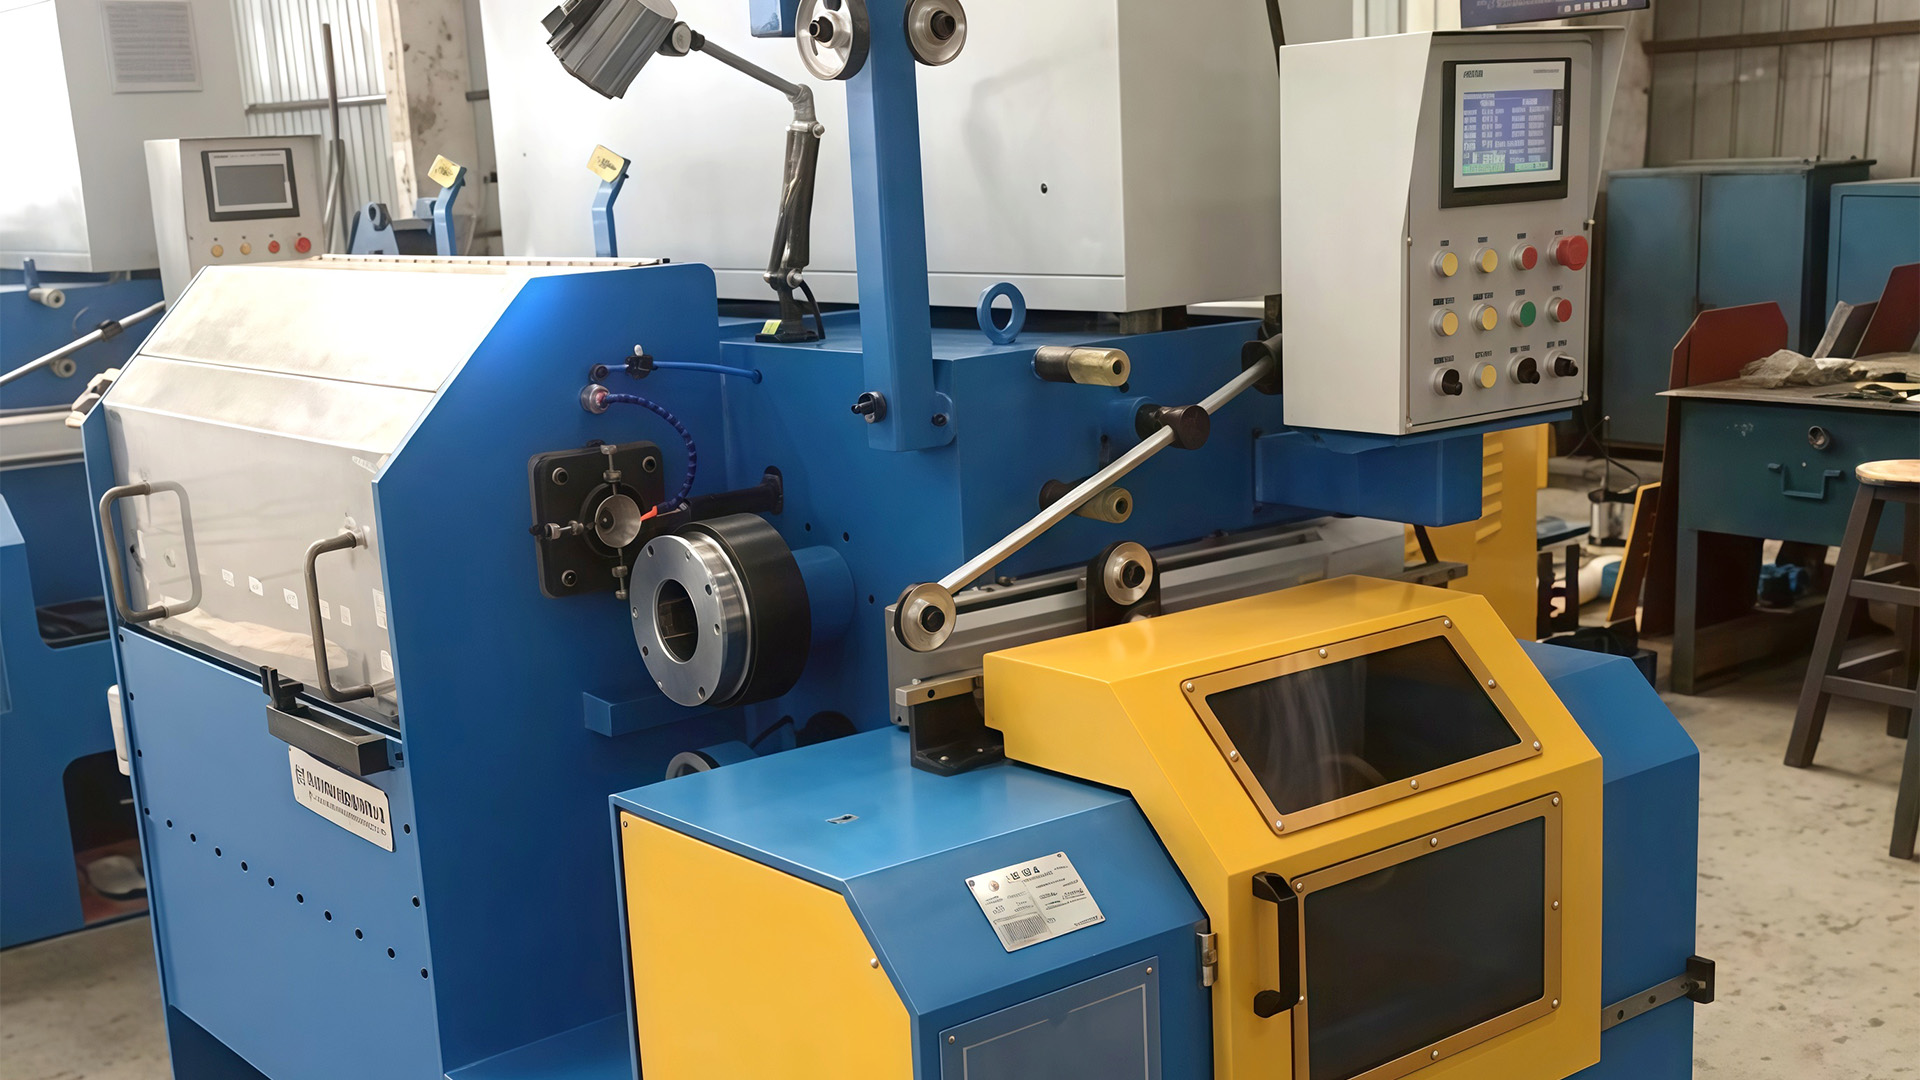
A line built for this duty pairs a water tank wire drawing machine layout with a die count chosen for the finished diameter rather than the machine's theoretical maximum.
Die Selection, Reduction Schedule and Tooling Tolerance
Dies are the cheapest part of the order and the most common cause of a rejected coil. On stainless, a die that is geometrically correct for low-carbon wire will polish unevenly, wear at the bearing and start leaving a faint spiral mark that the customer sees under a magnifier.
- An approach angle matched to the reduction taken in that pass, so the work is done in compression instead of at the bearing.
- A bearing length long enough to size the wire and short enough to avoid friction heat.
- A polished bore, because roughness introduced at the die is transferred to the wire surface immediately.
- Correct seating in the holder; a die sitting a fraction off axis will pull the wire oval.
- A regrinding and spares plan, since stainless wears tooling faster than low-carbon wire at the same gauge.
If a supplier cannot tell you the pass schedule the machine was quoted with, the die count in the offer is a guess.
Pay-off, Tension and Take-up: Where Consistency Is Won
Defects introduced before the final die are permanent, but so are defects introduced after it. A take-up that pulls unevenly, or a pay-off that lets the incoming wire surge as a coil unwinds, shows up as diameter variation, loose layers and a spool the customer cannot run at steady speed.
Tension control is best judged through a speed change. Accelerating from 200 to 600 m/min and back should not shift wire tension enough to move the diameter outside tolerance, and the answer is visible in the first hundred metres of a trial spool.
Spool Geometry and Traverse
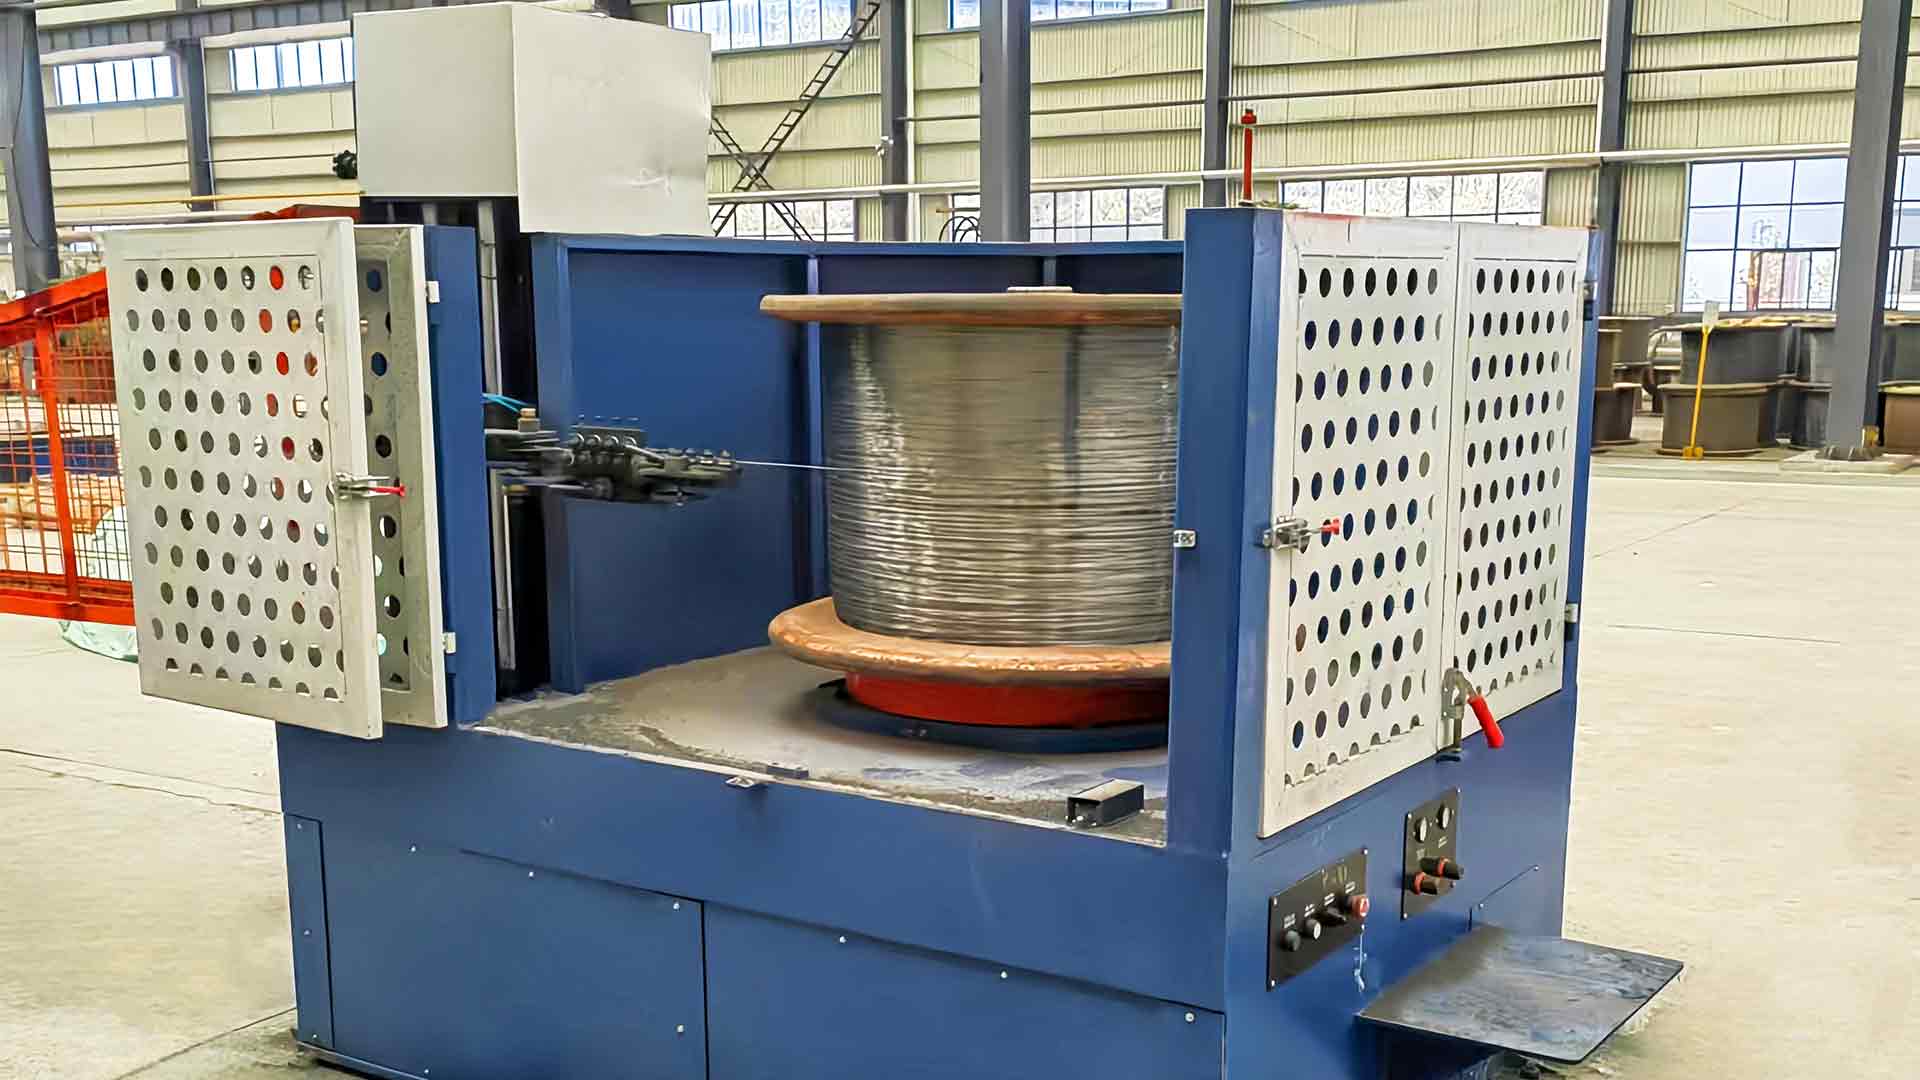
Traverse pitch and spool runout matter more on fine stainless than on heavier carbon wire. A spool wound with overlapping layers pays off in surges at the next process, and the drawing line usually gets the blame. Ask how the take-up is matched to your spool type, and check that the machine stops cleanly instead of dragging the wire after a break.
The same logic applies when sizing the winder: this guide to take-up machine selection covers spool types, tension matching and the efficiency numbers that matter.
Controls, Interlocks and the Numbers Worth Asking For
Control specification is where two machines that look identical on the factory floor begin to behave differently. The variables to pin down are the speed at which the machine is actually rated, the drive response to a load change, and what happens in the seconds after a wire break.
Watch for this: a quoted line speed measured with a short die sequence or without the finishing die fitted. Add the passes stainless genuinely needs and the real speed can fall by a third, which changes the economics of the whole line.
Put these in writing before the order is confirmed:
- Rated speed at the final die, with the full stainless pass schedule fitted.
- Capstan diameter, surface finish and cooling arrangement.
- Emulsion flow per die position, sump volume and temperature control range.
- Filtration rating and how often elements are changed.
- Tension accuracy and behaviour during acceleration and deceleration.
- Braking time after a break, and the length of wire scrapped each time.
- Motor rating and drive type per capstan.
Matching the Machine to the Wire You Actually Sell
Stainless covers a wide range of products, and the drawing machine that suits 4 mm fastener wire is not the one that suits 0.15 mm braiding wire. The finished diameter decides the drawing method, the die count and the take-up.
- Spring, rope and hose reinforcement wire in the 0.2 to 1.0 mm range is drawn wet, with a long die sequence and light passes.
- Wire mesh and weaving wire needs roundness and a consistent surface more than it needs maximum speed.
- Cable and stranded conductor work is sensitive to tension stability, because diameter variation reappears at the stranding stage.
- Fasteners, screws and formed parts are usually drawn from heavier stainless rod, where dry drawing and capstan cooling dominate.
- Welding wire adds cleanliness requirements, which puts filtration and lubricant chemistry back at the centre of the decision.
Across all of these, the features above stay the same. Only the emphasis shifts: die and cooling geometry for fine wire, tension and take-up for wire that is spooled, drive and capstan design for heavier rod.
Stainless steel wire drawing is less forgiving than low-carbon drawing, and the reason is metallurgical rather than mechanical. Work hardening, heat at the die and surface sensitivity turn small design decisions into visible defects on the coil.
The features worth paying for are submerged die cooling, a filtered and temperature-controlled lubricant circuit, precisely aligned tooling and holders, genuine tension control, and a take-up matched to the spool your customers actually run. Everything else, headline speed included, is secondary.
Good sign: a supplier who asks for your material grade, final diameter and spool type before quoting a speed. That conversation is the shortest route to a machine that draws stainless well, and it usually separates a line that holds tolerance from one that is adjusted every shift.